
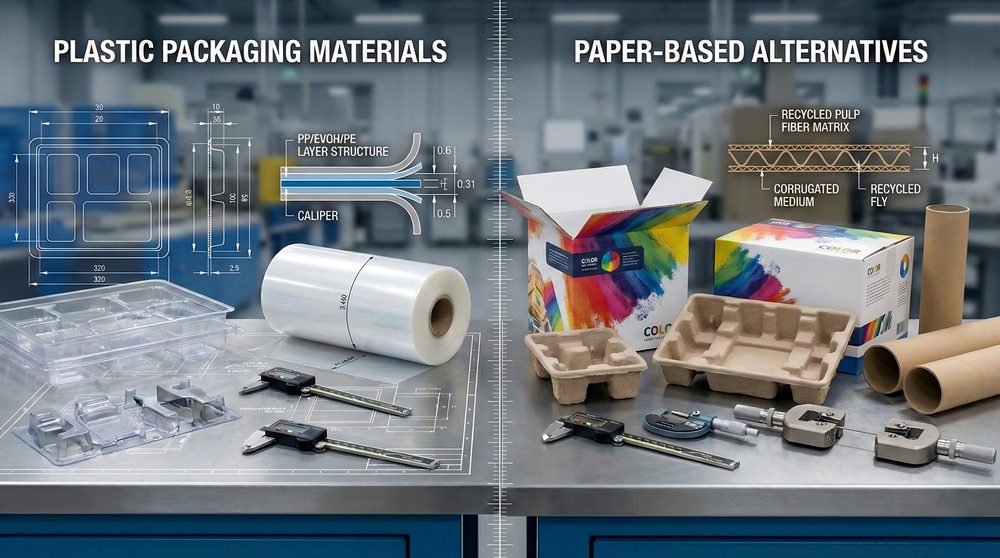
Plastic-Free Packaging:
How Brands Transition from Plastic to Paper Alternatives
Plastic-free packaging is becoming a strategic design choice for brands facing changing packaging rules, customer requirements, and waste-reduction targets. However, regulations do not universally require all packaging to be plastic-free.
This guide explains how to evaluate paper-based alternatives, manufacturing feasibility, protective performance, compliance requirements, and total cost before committing to production.
Table of Contents
Executive Summary: The 60-Second Decision Framework
Myth vs. Reality: Plastic-Free Means Redefining What “Works”
Plastic-free packaging is usually a structural redesign project, not a material replacement project.
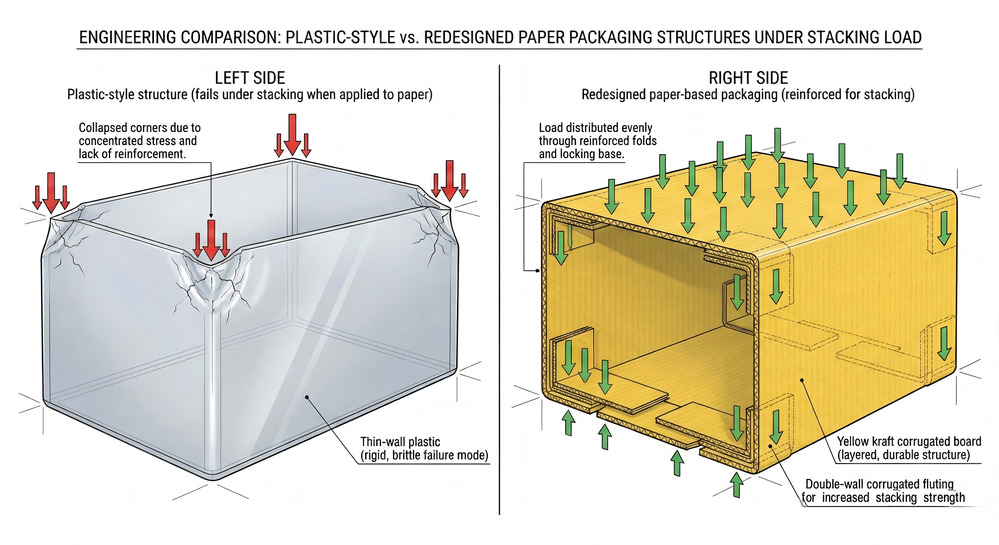
Plastic-free packaging is not a material swap.
It requires structural redesign so packaging can still run at line speed, stack safely, and survive transport.
The real decision is not “which paper,” but whether these two inputs are aligned:
- Paper strength direction (MD/CD)
- Required packaging strength (pallet stacking, transport load, drop risk)
When plastic geometry is reused, the outcomes are predictable:
- Collapsed stacks or corner instability
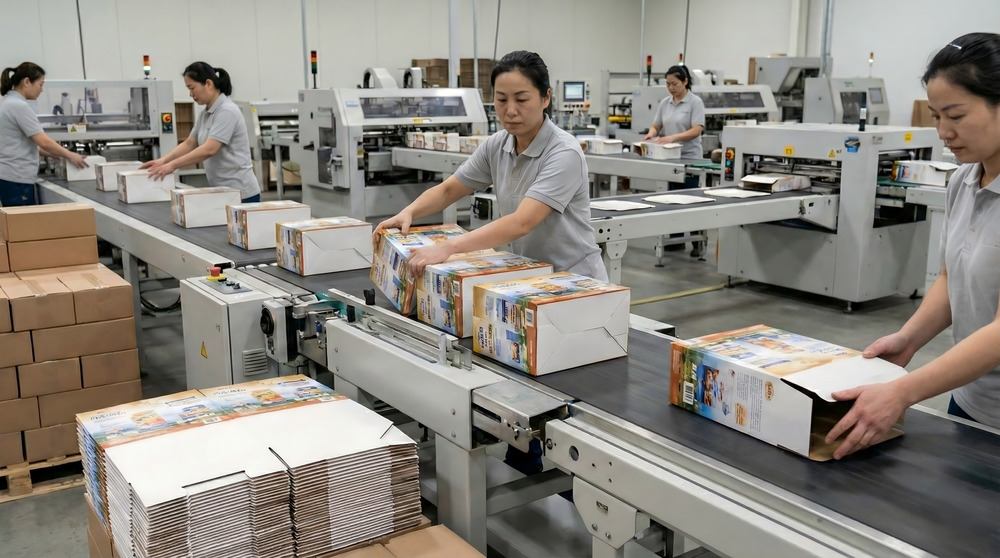
- Trial runs that pass, but mass production forces slower line speed
- Last-minute thickening, reinforcement, or full structural rework
Humidity changes during shipping and storage can expose weaknesses in material selection, structural design, adhesives, or manufacturing controls. The root cause should be investigated rather than assumed.
Regulatory Timelines: Why Packaging Decisions Need Earlier Planning
EU packaging requirements are changing, but different obligations follow different timelines. The PPWR began applying on 12 August 2026, with further requirements phased in over subsequent years. The EUDR has separate product-scope and implementation rules. Brands should confirm which requirements apply before changing materials or making compliance claims.
When documentation, structure, or material definitions are unclear, risk turns into:
- Urgent proof requests
- Shipment holds or clearance delays
- Blocked access to certain markets or channels
Late action narrows options, compresses timelines, and increases cost.
Executive Logic: Three Conditions Must Hold at the Same Time
Every plastic-free decision sits between three forces:
- Cost: material price, line speed impact, and rework risk
- Compliance: whether proof can be produced quickly during checks or audits
- Consumer acceptance: whether the change is understood, valued, and not questioned
The first two determine whether the solution works.
The third determines whether it is worth scaling.
If only one action is taken first, it should be locking strength targets and structure so the solution runs—before refining materials or messaging.
In 2026, the real barrier is not material choice, but structure, documentation, and decision timing.
Delays are more expensive than technical difficulty.
Execution matters more than perfection.
The 2026 Compliance Landscape: Avoiding the 3 Most Expensive Errors
The “Paper-is-Enough” Error: Proof Matters More Than Paper
Switching from plastic to paper does not automatically make packaging compliant.
Near the 2026 enforcement window, the real risk is not material failure. It is paperwork failure.
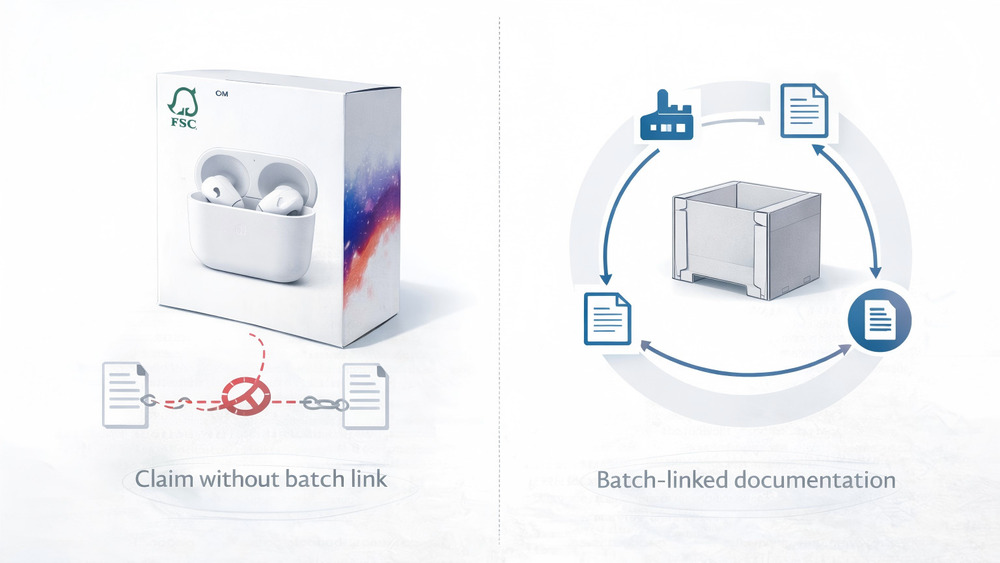
The EU Deforestation Regulation (EUDR) applies to relevant commodities and products within its legal scope, subject to applicable implementation dates. Paper-based packaging is not automatically covered merely because it contains paper. Buyers should first verify product classification, their role in the supply chain, and applicable due-diligence obligations.
FSC certification or chain-of-custody documentation may support specific sourcing claims, but neither automatically establishes EUDR compliance. Where documentation is required, the evidence must match the relevant product, certified claim, transaction, and applicable regulatory requirements.
Paper opens the door.
Proof keeps it open.
The “Tax Blindspot”: Structure Drives EPR Risk
EPR (Extended Producer Responsibility) is not just a material tax.
It shifts packaging reporting and waste costs to the party placing products on the market.
The common mistake is assuming paper automatically lowers risk or cost.
In reality, EPR exposure is shaped by structure:
- Multi-material packs increase reporting complexity.
- Hard-to-separate components raise long-term fees.
- Multiple SKU versions create data mismatches.
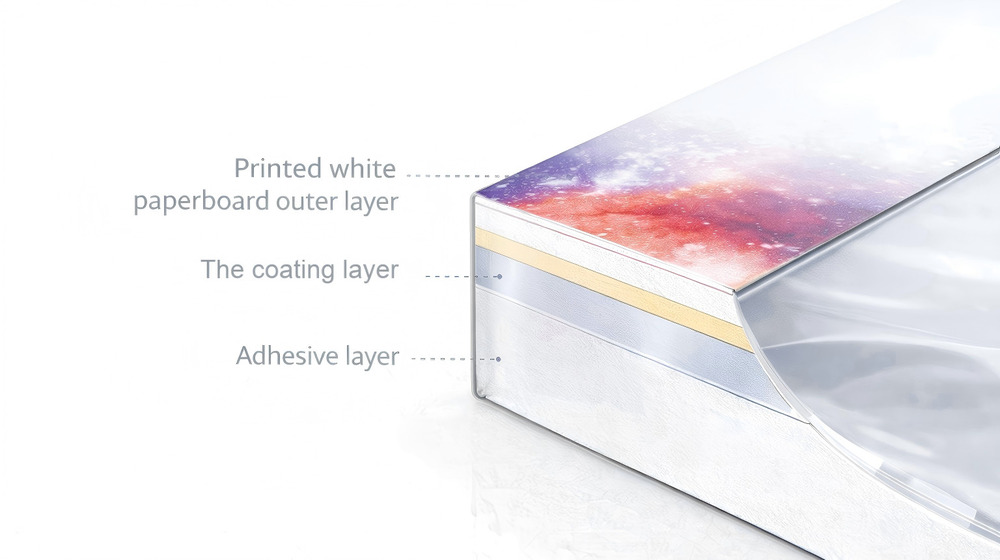
If structure and documentation drift apart, reporting becomes messy fast.
Start early.
Build a packaging BOM.
Control versions like you control artwork.
The “Border Check” Reality: PPWR Raises the Minimum Bar
PPWR (Packaging and Packaging Waste Regulation) sets clearer, stricter packaging rules across the EU.
It does not change how every country recycles.
But it does raise the minimum bar for what qualifies as acceptable packaging.
The EU Packaging and Packaging Waste Regulation (PPWR) has applied since 12 August 2026, with additional obligations taking effect on different schedules. It addresses packaging waste, minimization, recyclability, and other requirements—not a universal ban on plastic packaging.
What does that mean in practice?
Structure and documentation must match.
Grey-zone designs must be explainable.
Supply chain changes must trigger document updates.
Most shipment problems do not start at the border.
They start months earlier, when a small structural change was never reflected in the paperwork.
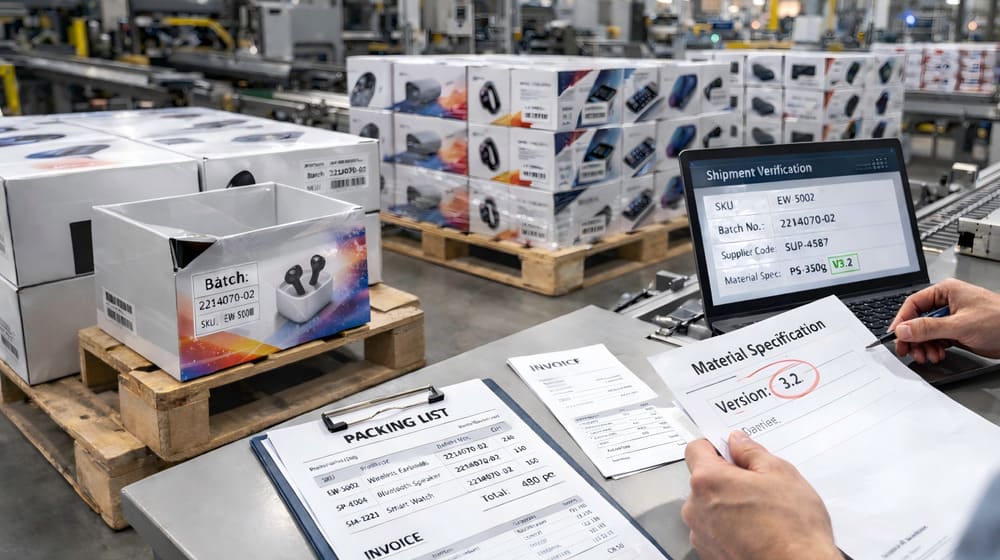
By 2026, the expensive compliance failures will not come from choosing the wrong material.
They will come from letting packaging move into mass production without managing it as a controlled specification.
Changes in packaging structure, materials, suppliers, or documentation can create compliance and audit risks when records no longer match the actual product. These risks should be reviewed before production approval rather than discovered during shipment or customer verification.
If you do only one thing, lock structure version, supply chain version, and document version together.
That discipline reduces compliance risk more than switching materials alone.
Understanding “Plastic-Free” in 2026: Beyond the Marketing Claims
Hidden Plastics: What “Plastic-Free” Often Hides
Many packages labeled “plastic-free” still contain plastic components.
Common examples include:
- PE film lamination
- Plastic window patches
- Certain synthetic adhesives or barrier layers
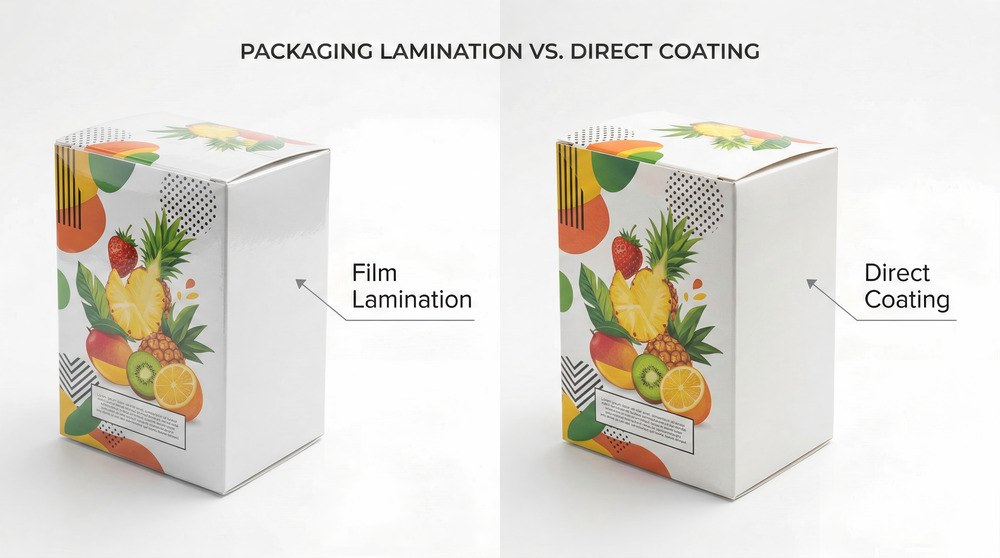
The real question is not how much plastic is present.
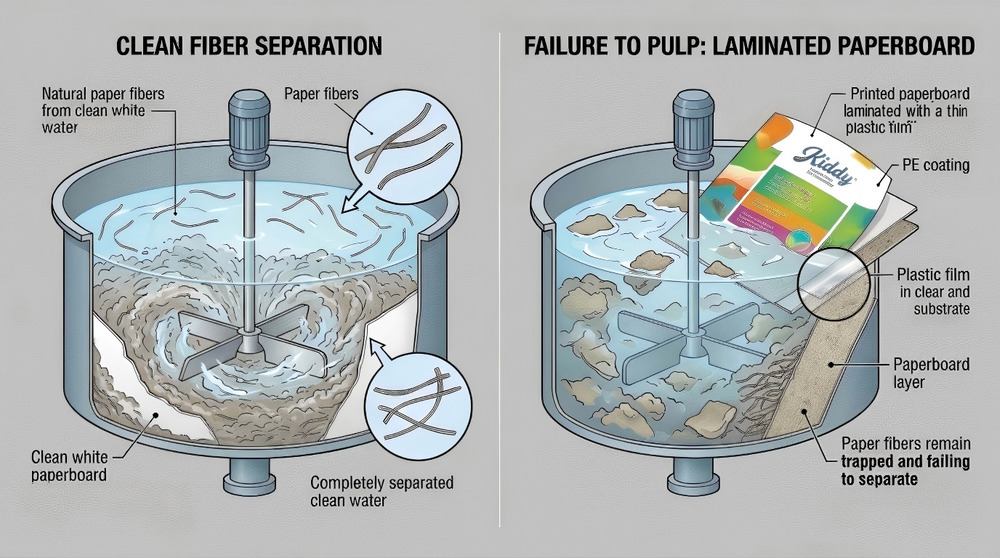
It is whether the structure interferes with paper repulping.
In recycling facilities, used paper is pulped in water so fibers can separate.
If coatings or films block that process, the packaging may not be accepted.
Film lamination is not explicitly banned in mainstream markets.
Recyclability depends on how the structure performs within local recycling systems.
If lamination reduces fiber recovery or lowers recyclability classification, it may face increasing compliance pressure over time.
The issue is not the material label.
It is structural performance.
Repulpable vs. Biodegradable: Know the Difference
Biodegradable means a material can break down under certain conditions.
Repulpable means it can be processed in a paper mill and turned back into fiber.
For most paper retail packaging, recycling systems care about repulpability, not biodegradation.
If a structure cannot release fibers during pulping,
a biodegradable claim does not solve the recycling issue.
Verification: What Is Reasonable to Ask For
You do not need complex certifications.
But when a supplier claims plastic-free or recyclable, ask for:
- Clear material specifications (coating type, film presence)
- MSDS or environmental compliance reports (such as REACH or RoHS)
- Evidence if repulpability is claimed
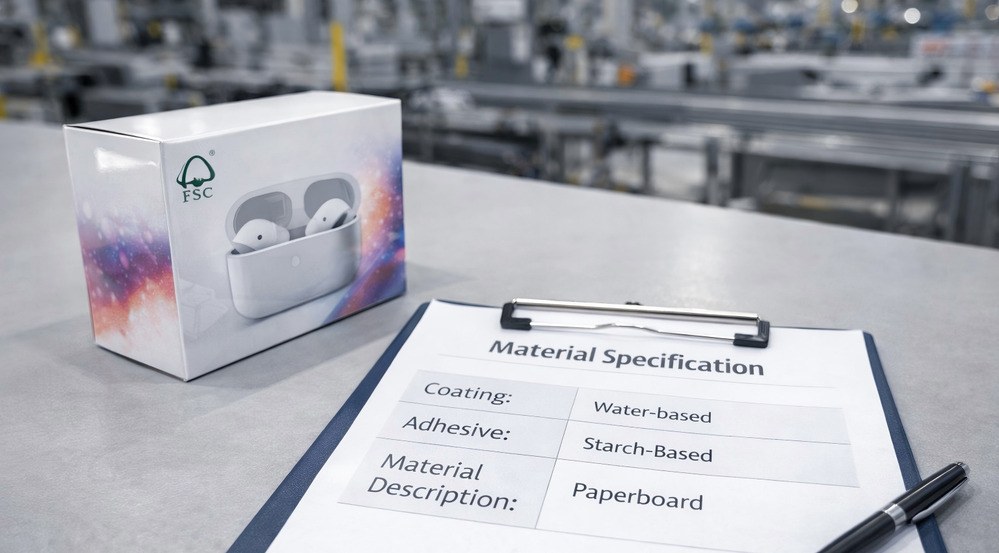
The issue is not the number of documents.
It is whether they match the actual structure used.
In real projects, the risk around “plastic-free” usually comes from structural behavior, not the label.
Many export packages still use lamination because it balances cost and appearance.
The issue is not its existence, but understanding how it performs in recycling systems.
The real test is whether the structure can enter the circular system—not whether it sounds sustainable.
Paper-Based Alternatives: What Actually Works at Scale
Paperboard / Corrugated: When You Must Redesign
Moving from plastic to paper is not a material swap. It is a structural redesign.
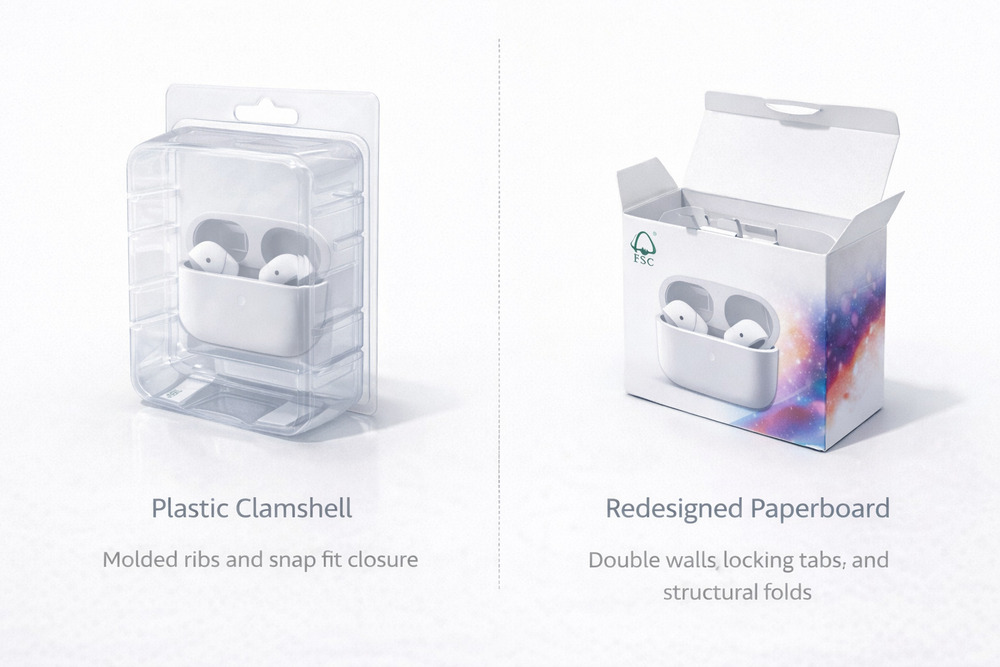
Redesign is usually required when:
- The original pack relied on plastic snap-fit or flexibility
- Strength came from molded ribs
- Stacking pressure is high
- Automation is sensitive to tolerance
Paper builds strength through folds, overlaps, and controlled load paths.
Copying plastic logic leads to production problems.
For simple product cavities, a folded paperboard insert may follow the basic layout of an existing EVA or plastic insert. More complex cavities usually require structural adjustments because folding, locking, and support geometry differ from molded plastic or foam. The redesign should be checked against the actual product rather than judged by appearance alone.
Molded Pulp: Tooling Cost and Production Reality
Both dry-press and wet-press molded pulp rely on tooling.
This means:
- Not suitable for low volumes due to mold cost
- Not ideal for urgent timelines
Molded pulp development requires separate tooling and approval stages. Sample molds typically take 12–15 days. Production mold development and preparation for the first mass-production run may require approximately 20–25 days, depending on project complexity and approval timing. These figures are planning references, not a guaranteed combined project lead time.
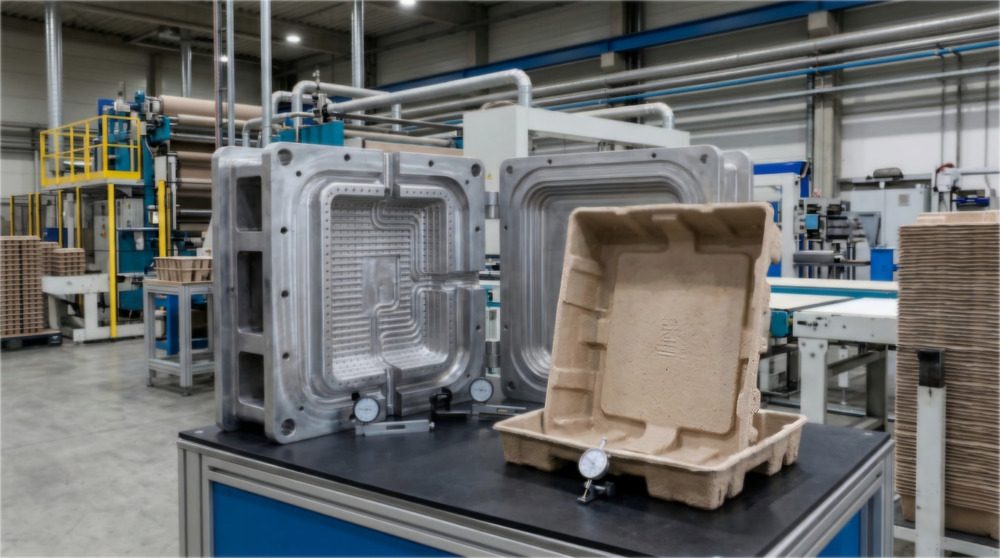
Molded pulp can reproduce much of an existing insert's cavity geometry through tooling, but it is not a direct performance equivalent to EVA or plastic. Edge clearances, contact points, cushioning space, wall geometry, and outer-carton fit may need adjustment to preserve the intended protection.
At Klong, we don't treat molded pulp as a drop-in replacement for EVA foam. Tooling can reproduce much of the original cavity shape, but edge clearances, support points, and cushioning space still need attention. A cavity that looks identical doesn't necessarily protect the product in the same way.
For fit:
- Do not aim for zero clearance
- Leave molding tolerance
- Large formats must consider cushioning and outer carton fit
A good sample fit does not guarantee stable production.
Barrier-Coated Papers: A Direction, Not a Shortcut
Barrier-coated paper uses a functional coating to improve grease or moisture resistance.
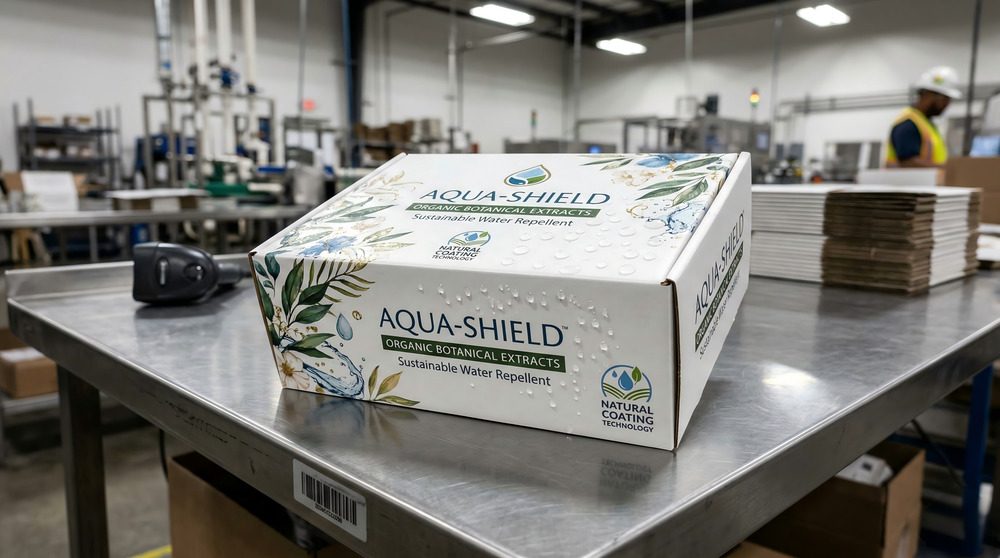
The goal is to reduce reliance on plastic film while keeping a paper-based structure.
These materials are increasingly requested in food and cold-chain packaging.
However:
- Barrier performance is usually lower than multi-layer plastic films
- Different coatings affect recyclability differently
- It is not a full replacement in every case
For future projects, a practical approach is:
- Source specialized barrier-coated paper suppliers
- Confirm recyclability compatibility with the target market
It is not a universal solution, but it is a viable direction when properly evaluated.
Paper-based alternatives succeed at scale when structural limits are understood.
Paperboard and corrugated require load-path redesign.
Molded pulp requires tooling and timeline planning.
Barrier-coated paper requires performance and recyclability checks.
Stability comes from defining constraints first, then selecting the structure.
Performance Comparison: Paper-Based Alternatives vs. Traditional Plastic
Protection Metrics: What Really Changes
Switching to paper does not automatically reduce protection.
But the load logic changes.
Plastic relies more on material flexibility.
Paper relies on structure to distribute force.
In paper-based packaging, focus on:
- Burst strength
- Edge crush strength (ECT)
- Stacking load paths
- Moisture impact for sensitive goods
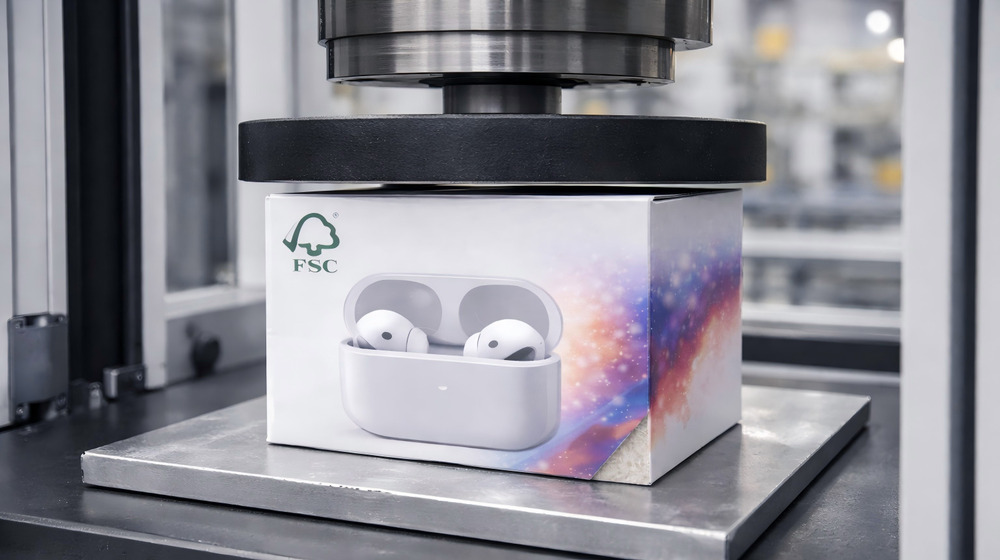
Most failures are not caused by “thin paper.”
They happen when:
- Folds become stress points
- Inserts and cartons carry load differently
- Stacking was never recalculated
Paper protects when the structure carries the load correctly.
Automation Speed: Why Lines Slow Down
Plastic is more forgiving on high-speed lines.
Paperboard is not.
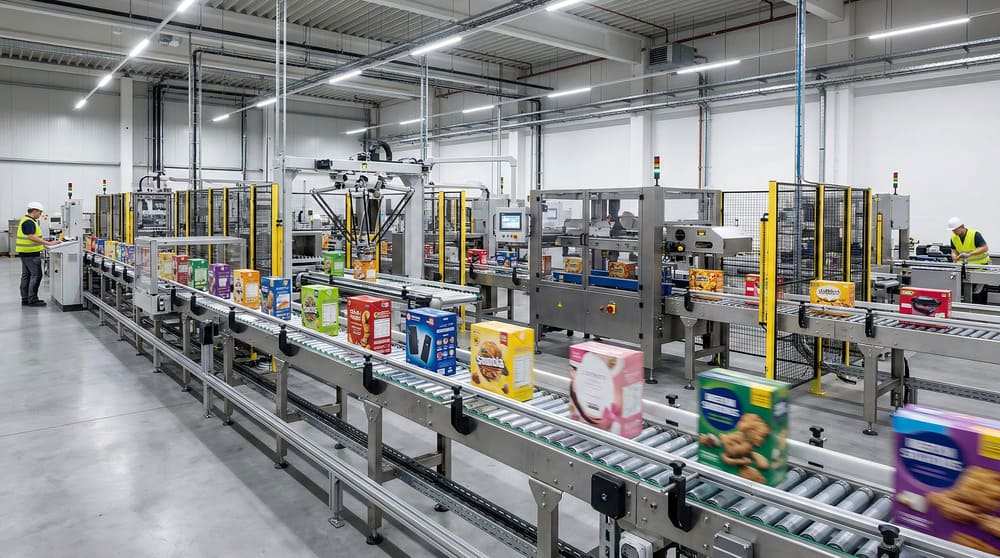
Slowdowns usually come from:
- Unstable surface friction
- Inconsistent opening angles
- Tabs that are too tight or too loose
- Limited spring-back after folding
The goal is not “it runs once.”
It’s “it runs consistently.”
Designing for automation early prevents speed loss.
The Humidity Challenge: Prove It with Real Testing
Paper is moisture-sensitive. That’s true.
But testing does not need to become a lab project.
For typical export packaging:
- Run a drop test to confirm impact strength
- Run temperature or humidity cycling to simulate transport conditions
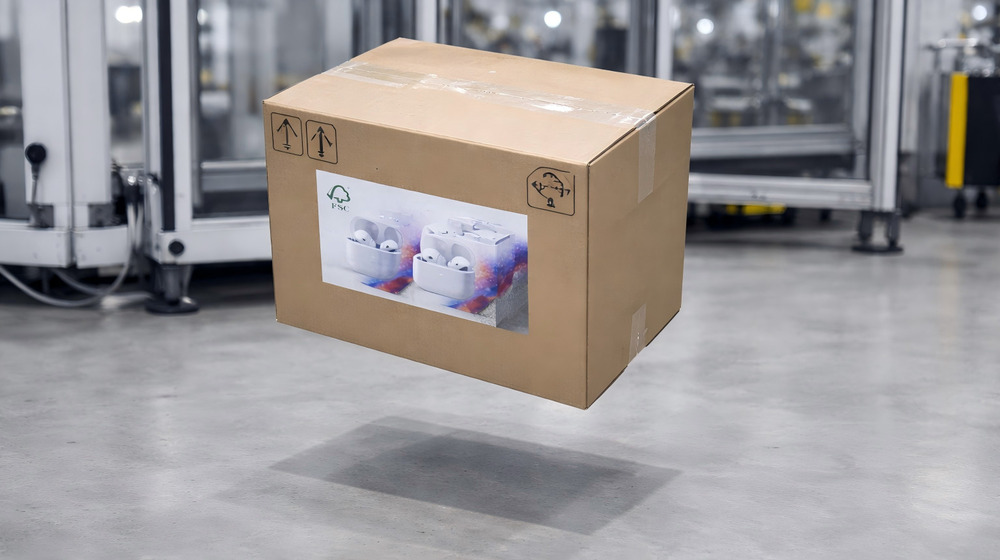
Passing a drop test or environmental screening does not guarantee performance across every distribution route. Validation should reflect product fragility, packaging configuration, stacking exposure, shipping conditions, and customer-specific acceptance criteria.
Paper-based alternatives should be approved against defined protection requirements, with additional testing arranged when identified risks justify it. A successful test supports the approval decision only within its agreed scope and conditions.
Suitability Boundaries: When Plastic-Free Is the Wrong Choice
High Grease, Long Shelf Life, and Cold-Chain Products
Not every product is ready for an immediate plastic-free transition.
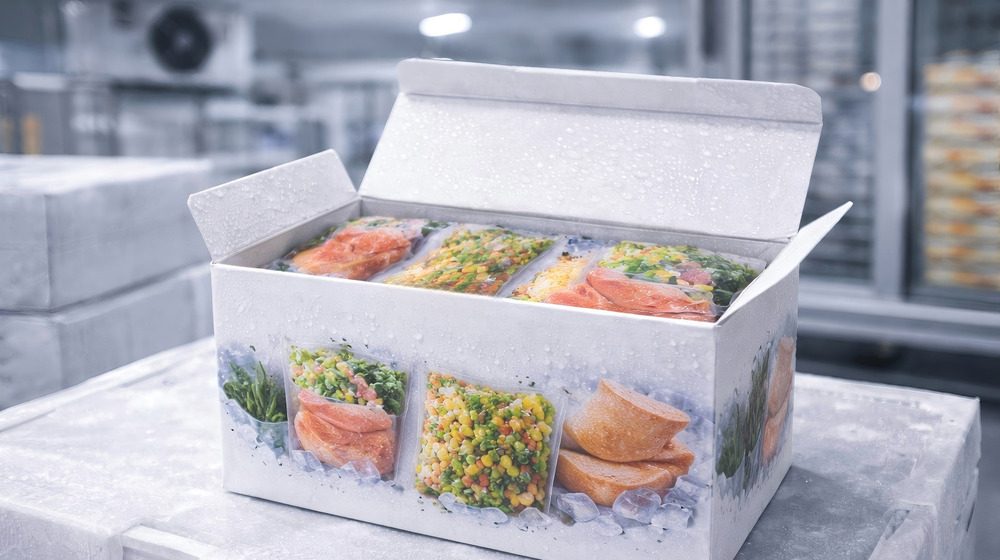
High-grease foods, cold-chain meat products, and long shelf-life items require careful evaluation.
The reasons are practical:
- Grease migration is continuous
- Moisture control requirements are higher
- Temperature differences affect material stability
Some barrier-coated papers may experience performance changes after folding and forming.
Over long storage periods, even small differences can become significant.
If the product relies heavily on plastic film for grease or moisture protection,
a full paper conversion should be validated before implementation.
In these cases, a phased transition or hybrid structure is often more realistic.
Sustainability goals and product stability should be validated together.
High-Speed Lines with Zero Downtime Tolerance
On high-speed automated lines, structural stability often takes priority.
When line speed is high and downtime costs are significant,
changes in friction, tolerance, or opening consistency can affect efficiency.
If the current plastic format runs reliably,
a paper redesign should verify:
- Surface friction stability
- Locking smoothness
- Achievable line speed
Without sufficient testing time,
a phased transition is usually more controllable than a full replacement.
Sustainability targets can be scheduled.
Production stability must be maintained.
When Compliance Goals and Product Risk Are Out of Balance
Some regulations define clear timelines,
but many transitions also include phased implementation.
If a replacement is implemented without validating product stability,
risk may shift toward returns or claims.
A more balanced path includes:
- Replacing lower-risk SKUs first
- Running focused validation on higher-risk products
- Keeping structure and documentation aligned
Compliance and product stability should progress together.
In real projects, risk often comes from timing rather than material alone.
When a structure must resist grease, moisture, or high-speed stress,
replacement decisions should follow validation.
Defining the boundary is part of professional judgment.
A 5-Step Transition Path: How to Execute without Production Downtime
Step 1 — Map Plastic Components and Estimate Cost Range
Do not redesign first. Gain visibility.
Map all plastic-related components:
- Window films
- Tapes
- Inserts
- Labels
- Transport materials
Estimate:
- Alternative materials
- Raw material impact
- Whether projected cost fits the acceptable range
Tooling cost mainly applies to molded pulp.
Die-cut cost for folding cartons is usually low.
If cost is unacceptable, adjust here before moving forward.
Step 2 — Low-Cost Structural Prototype
Structural development does not require heavy investment.
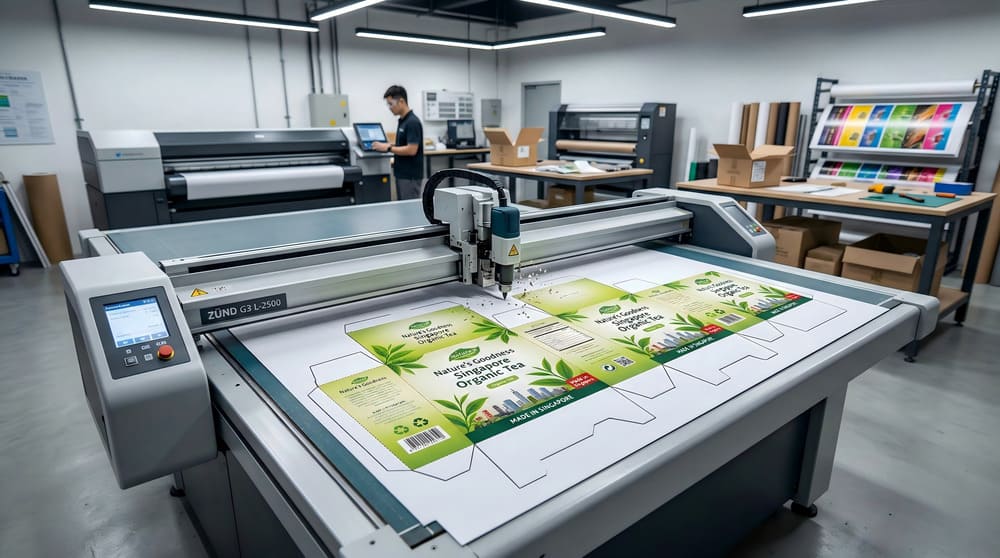
Except for molded pulp, most flat paper structures can be prototyped using a cutting plotter.
The goal:
- Optimize based on experience
- Confirm appearance
- Validate structural logic
Confirm feasibility before refinement.
Step 3 — Structural & Environmental Validation
Once direction is confirmed, run basic validation:
- Drop test
- Temperature or humidity cycling
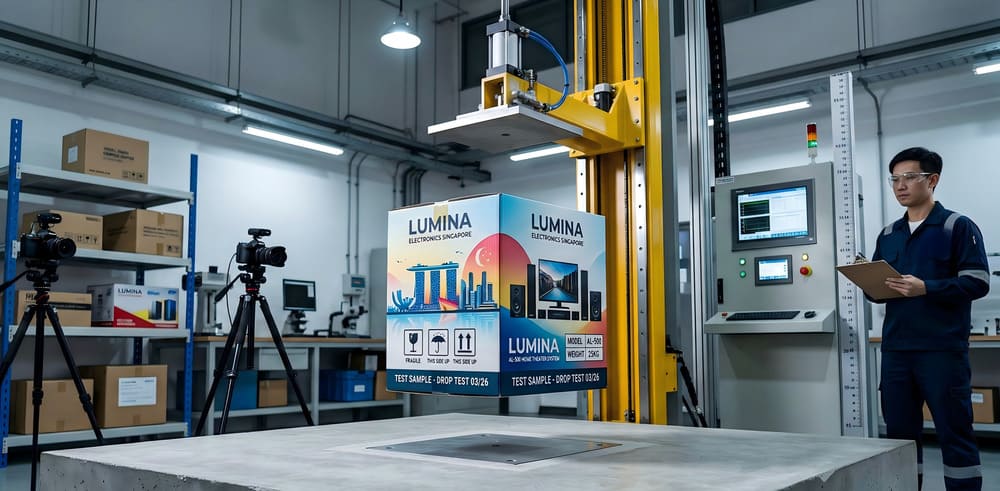
Check:
- Whether strength covers transport
- Whether performance drops significantly
If tests fail, return to redesign.
Step 4 — Sample Approval or Small Batch Trial
After validation, proceed with formal sample approval or a small batch trial.
For folding cartons, decide based on:
- Structural complexity
- Manual assembly involvement
Simple structure → sample sign-off may suffice.
Complex or labor-intensive → small batch trial is safer.
Extended automation testing is more common in pharmaceutical or very high-volume small cartons.
Confirm:
- Smooth production
- Stable locking
- Consistent appearance
Step 5 — Lock Versions and Confirm Final Cost
Before scaling, confirm:
- Material version
- Structure version
- Supplier source
- Documentation
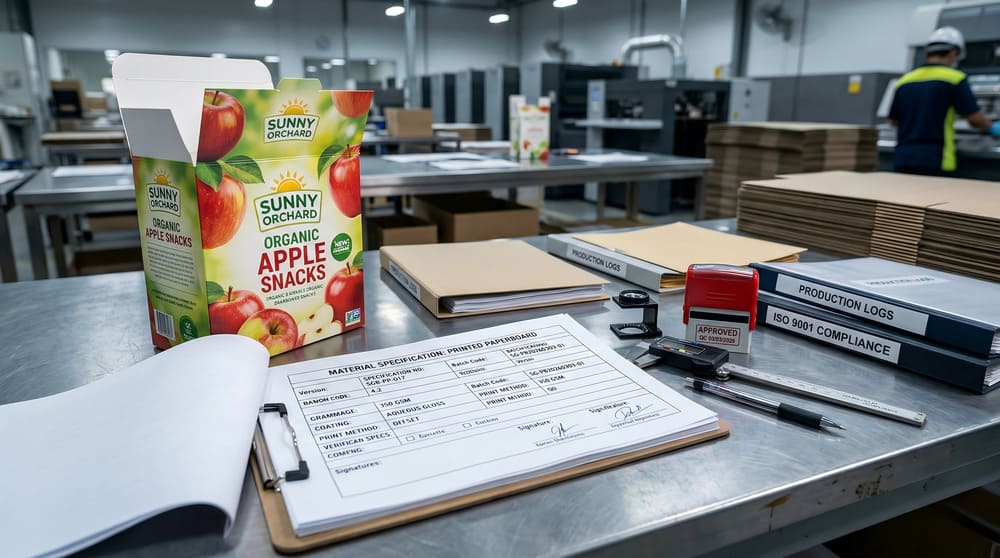
Ensure final cost aligns with the initial estimate.
The focus here is stability, not cancellation.
Scale after versions are locked.
Plastic-free transition does not require heavy upfront investment.
The sequence is clear:
- Screen cost early
- Prototype efficiently
- Validate basics
- Decide trial level by complexity
- Lock versions before scaling
Controlled pacing reduces risk.
Cost, Timeline, and Scale: The Real ROI of Going Plastic-Free
Total Landed Cost: What Changes Beyond Material Price
When buyers ask “how much will it cost,” they are rarely asking about paper price alone.
They want to know whether the transition will affect total cost and delivery stability.
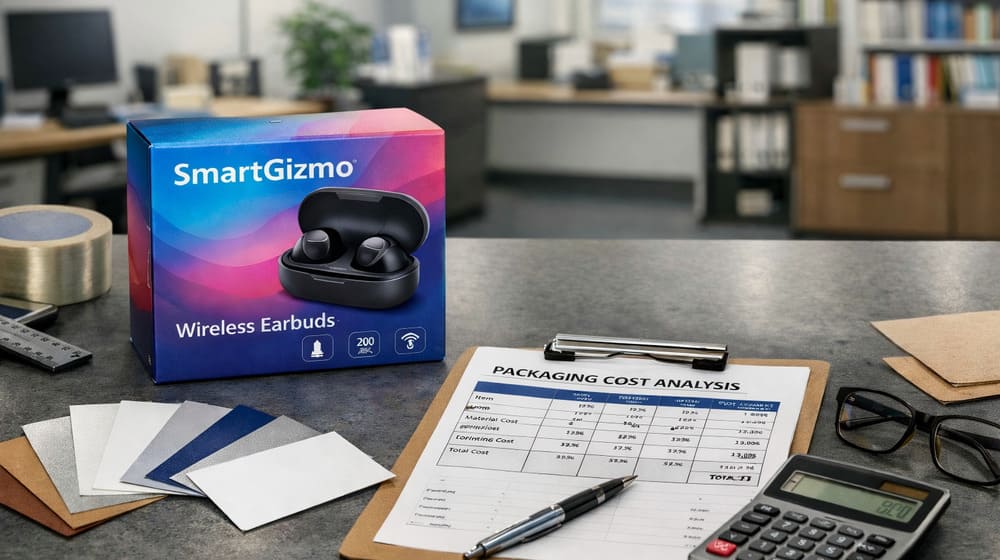
A practical view breaks the cost into three parts:
- Material and structure: board type, inserts, and added processes
- Compliance responsibility: market-related costs such as EPR
- Logistics and delivery: packing method, transport damage, and landed stability
Material price is only one part.
The real ROI is turning compliance into a predictable delivery cost instead of repeated rework.
The Productivity Shift: Line Speed and Manual Assembly
Productivity should be considered, but paper packaging is not automatically slower.
Forming efficiency should be a design constraint from the beginning, aiming to stay close to the original packing pace.
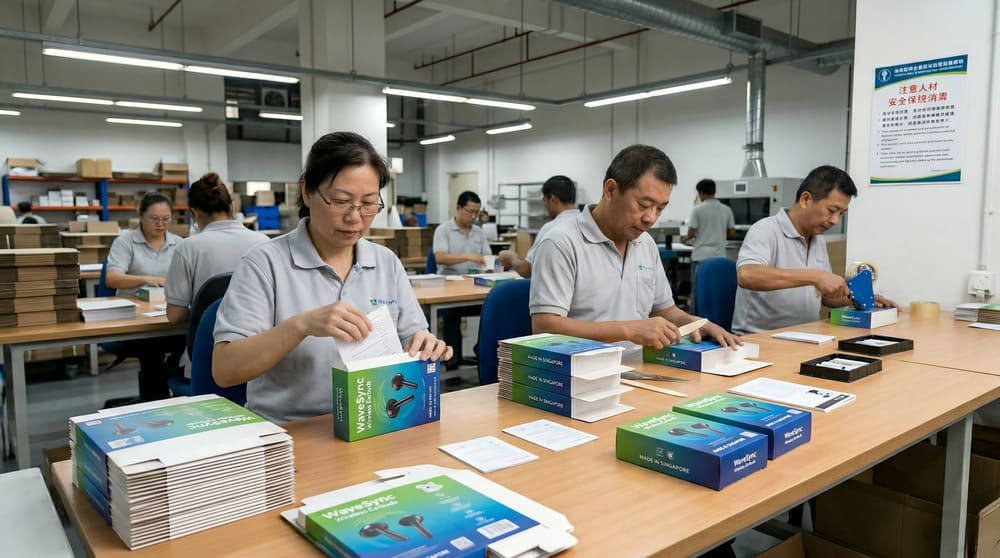
Two things should be checked early:
- Automation lines: for small cartons with very high volumes (such as pharmaceutical packaging), structures must be machine-friendly.
- Manual assembly: if packing is manual, reduce unnecessary actions such as excessive tabs or complex folding.
The goal is not to avoid paper, but to design for efficiency and confirm it during sampling.
Timeline Reality: How Long It Takes to Launch Safely
“Time to launch” often matters more than material price.
For standard folding carton and paper insert projects, structural samples typically take 5–7 days when standard materials are available and dedicated tooling is unnecessary. Printed or production-representative samples may require approximately 7–10 days, depending on the processes involved.
Molded pulp development requires a separate tooling schedule. Sample molds typically take 12–15 days, while production mold development and preparation for the first mass-production run may require approximately 20–25 days, subject to project conditions.
After specification approval, standard mass-production lead times are generally 10–30 days. Sampling, tooling, testing, revisions, and production scheduling should be evaluated separately; these durations are not a guaranteed total project timeline.
The ROI of plastic-free packaging is rarely about the material price itself.
What matters more is reducing uncertainty early:
clear prototypes, validation, small-batch confirmation, and a reliable cost range.
Buyers mainly want to know whether the change will affect shipment stability or compliance,
and whether it will add operational complexity.
When productivity targets, validation steps, and final specifications are clarified early,
production usually runs more smoothly.
Verification & Accountability: Who Proves **Plastic-Free Packaging**, and When?
First Check: Do These Regulations Apply to My Packaging?
Before worrying about compliance, ask yourself three simple questions.
Will my packaged product enter the EU market?
If so, first determine the applicable PPWR requirements, implementation dates, and the responsible economic operators. Separately, assess whether the EUDR covers the relevant commodity or product classification. Paper content alone does not establish EUDR applicability.
The PPWR concerns packaging and packaging waste, while the EUDR addresses deforestation-related obligations for products within its scope. These regulations require separate applicability assessments and should not be treated as a general mandate to eliminate every plastic component.
Will my product enter markets that operate EPR systems?
This includes many regions such as the EU, UK, France, Germany, Canada, and Australia.
In most cases, the brand owner or importer must:
- register packaging responsibility
- report packaging quantities
- pay recycling fees
You don’t need to memorize every regulation.
But you should know when these rules start affecting your packaging decisions.
Who Is Responsible: Brand, Importer, or Packaging Manufacturer
In many packaging projects, compliance problems are not caused by complicated laws.
They come from unclear responsibility.
In most cases:
Brand owners or importers
handle regulatory responsibilities such as:
- EPR registration and reporting
- EUDR due diligence
- PPWR compliance declarations
To do this, they need information such as:
- material sourcing
- packaging structure
- material compliance statements
Most of this information comes from packaging suppliers.
Packaging manufacturers
usually provide technical inputs such as:
- material sourcing information (such as FSC CoC)
- packaging BOM
- environmental declarations
- necessary test data
In simple terms:
The brand manages regulatory responsibility,
while the packaging supplier provides technical proof.
Minimum Compliance Setup: The Basic Documents I Should Have
Most packaging projects do not require a complex compliance system.
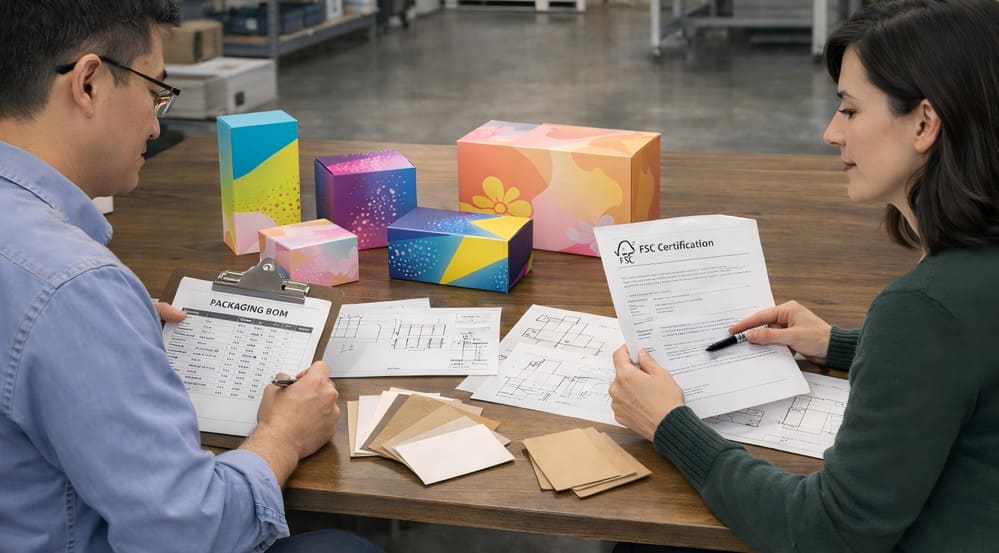
In practice, a basic documentation set usually includes:
- packaging BOM (bill of materials)
- material declarations or environmental reports (such as RoHS / REACH)
- FSC CoC information if certified paper is used
- packaging structure specifications or drawing versions
- shipment and order batch records
The goal is not to collect many documents.
The goal is to ensure these documents match a specific product and shipment batch.
Before Mass Production: Lock the Version Chain
During packaging development, structural changes are normal.
But before mass production starts, four things should be clear:
- structure version
- material version
- supplier source
- document version
These should also map clearly to:
SKU ↔ BOM
BOM ↔ batch
batch ↔ shipment
This makes it much easier to respond if a customer audit or inspection happens.
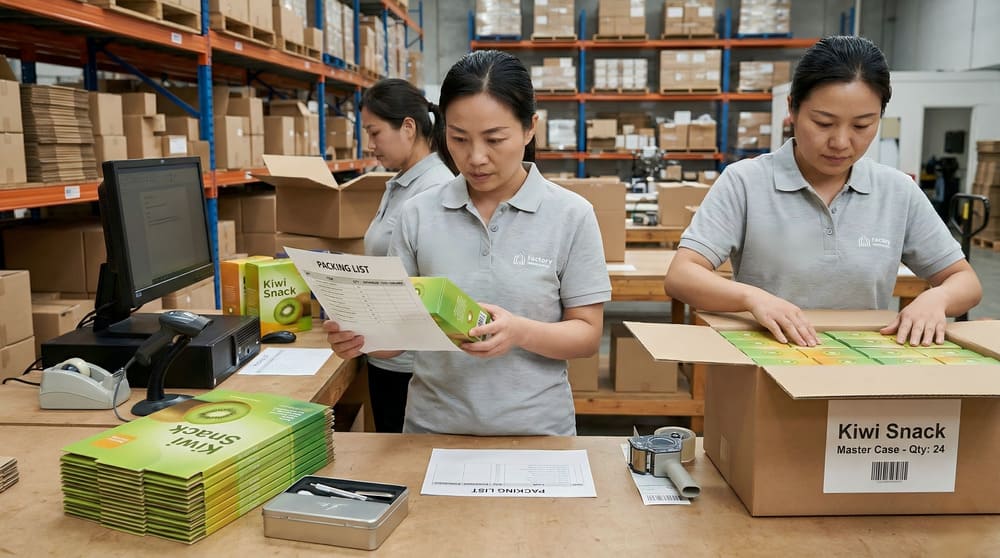
Packaging documentation can become unreliable when the approved structure, material source, or supplier changes without corresponding updates to specifications and supporting records. Before production release, buyers should confirm that the packaging BOM, drawing revision, relevant declarations, and batch identification reflect the actual approved configuration.
Plastic-Free Packaging: 6 Questions Buyers Should Resolve Before Switching
Before replacing plastic components, buyers should evaluate structural feasibility, protection, total cost, and the evidence needed for their target markets.
1. Does switching to plastic-free packaging always increase total cost?
Not necessarily. Paper-based alternatives may change material cost, tooling investment, assembly time, shipping volume, and damage risk. Folded paperboard inserts can sometimes reduce tooling requirements, while molded pulp generally requires dedicated molds. Buyers should compare total landed cost rather than unit price alone and validate that any savings do not compromise product protection or production efficiency.
2. Can molded pulp reproduce the shape of an existing EVA or plastic insert?
Often, much of the original cavity geometry can be reproduced through molded pulp tooling. However, edge clearances, support points, cushioning space, and manufacturing tolerances may require adjustment. Simple cavities may also be suitable for folded paperboard inserts, while complex shapes often need redesign. Final selection should follow physical fit and protection validation, not visual similarity alone.
3. Does mono-material paper packaging automatically qualify as recyclable?
No. Using predominantly paper-based components may simplify material separation, but recyclability depends on coatings, adhesives, finishes, contamination, and the recycling systems available in the destination market. Plastic-free and recyclable are different claims. Buyers should verify the complete packaging structure and obtain suitable supporting evidence before making environmental or regulatory claims.
4. Can paper inserts or molded pulp protect fragile products as well as EVA foam?
They can be viable alternatives when designed for the product's weight, fragile areas, contact points, and expected distribution hazards. However, EVA, folded paperboard, and molded pulp respond differently to impact and compression. Structural samples should be evaluated with the actual product, followed by project-appropriate testing. No material substitution guarantees damage-free delivery without relevant validation.
5. Does the EU PPWR require every packaging component to be plastic-free?
No. The PPWR establishes requirements covering packaging waste prevention, minimization, recyclability, and other areas, with obligations taking effect on different schedules. It does not impose a universal plastic-free requirement on all packaging. Buyers should review the actual packaging configuration, destination market, and applicable obligations before deciding which plastic components need to be replaced.
6. What should buyers confirm before approving a plastic-free packaging transition?
Confirm product dimensions, weight, fragile areas, existing insert structure, expected shipping conditions, packing-line requirements, order volume, and applicable customer standards. For molded pulp, assess tooling and cavity clearances; for folded inserts, review assembly and locking behavior. A DFM review and physical sampling plan help identify whether the transition is manufacturable before committing to production tooling.
Plastic-Free Fails When Protection Is Assumed, Not Verified
A paper insert that looks like your old plastic one may not protect like it. Discovering that after mass production can mean damaged products, delayed shipments, and costly rework.
Download Klong’s Plastic-Free Packaging Transition Checklist
Check structural fit, cushioning risks, and validation requirements before approving production tooling.